
Language
Hot Keyword:
Author:KUNYUAN Machine Manufacturer TIME:2026-08-22
Calculate capacity on a declared time and fabric basis. Actual accepted kilograms per scheduled hour equals the accepted fabric mass attributed to the order divided by its scheduled hours. Keep a theoretical plain-jersey running rate beside this measured result, then explain stopped time, startup material and fabric disposition. Catalogue RPM alone cannot supply those records.
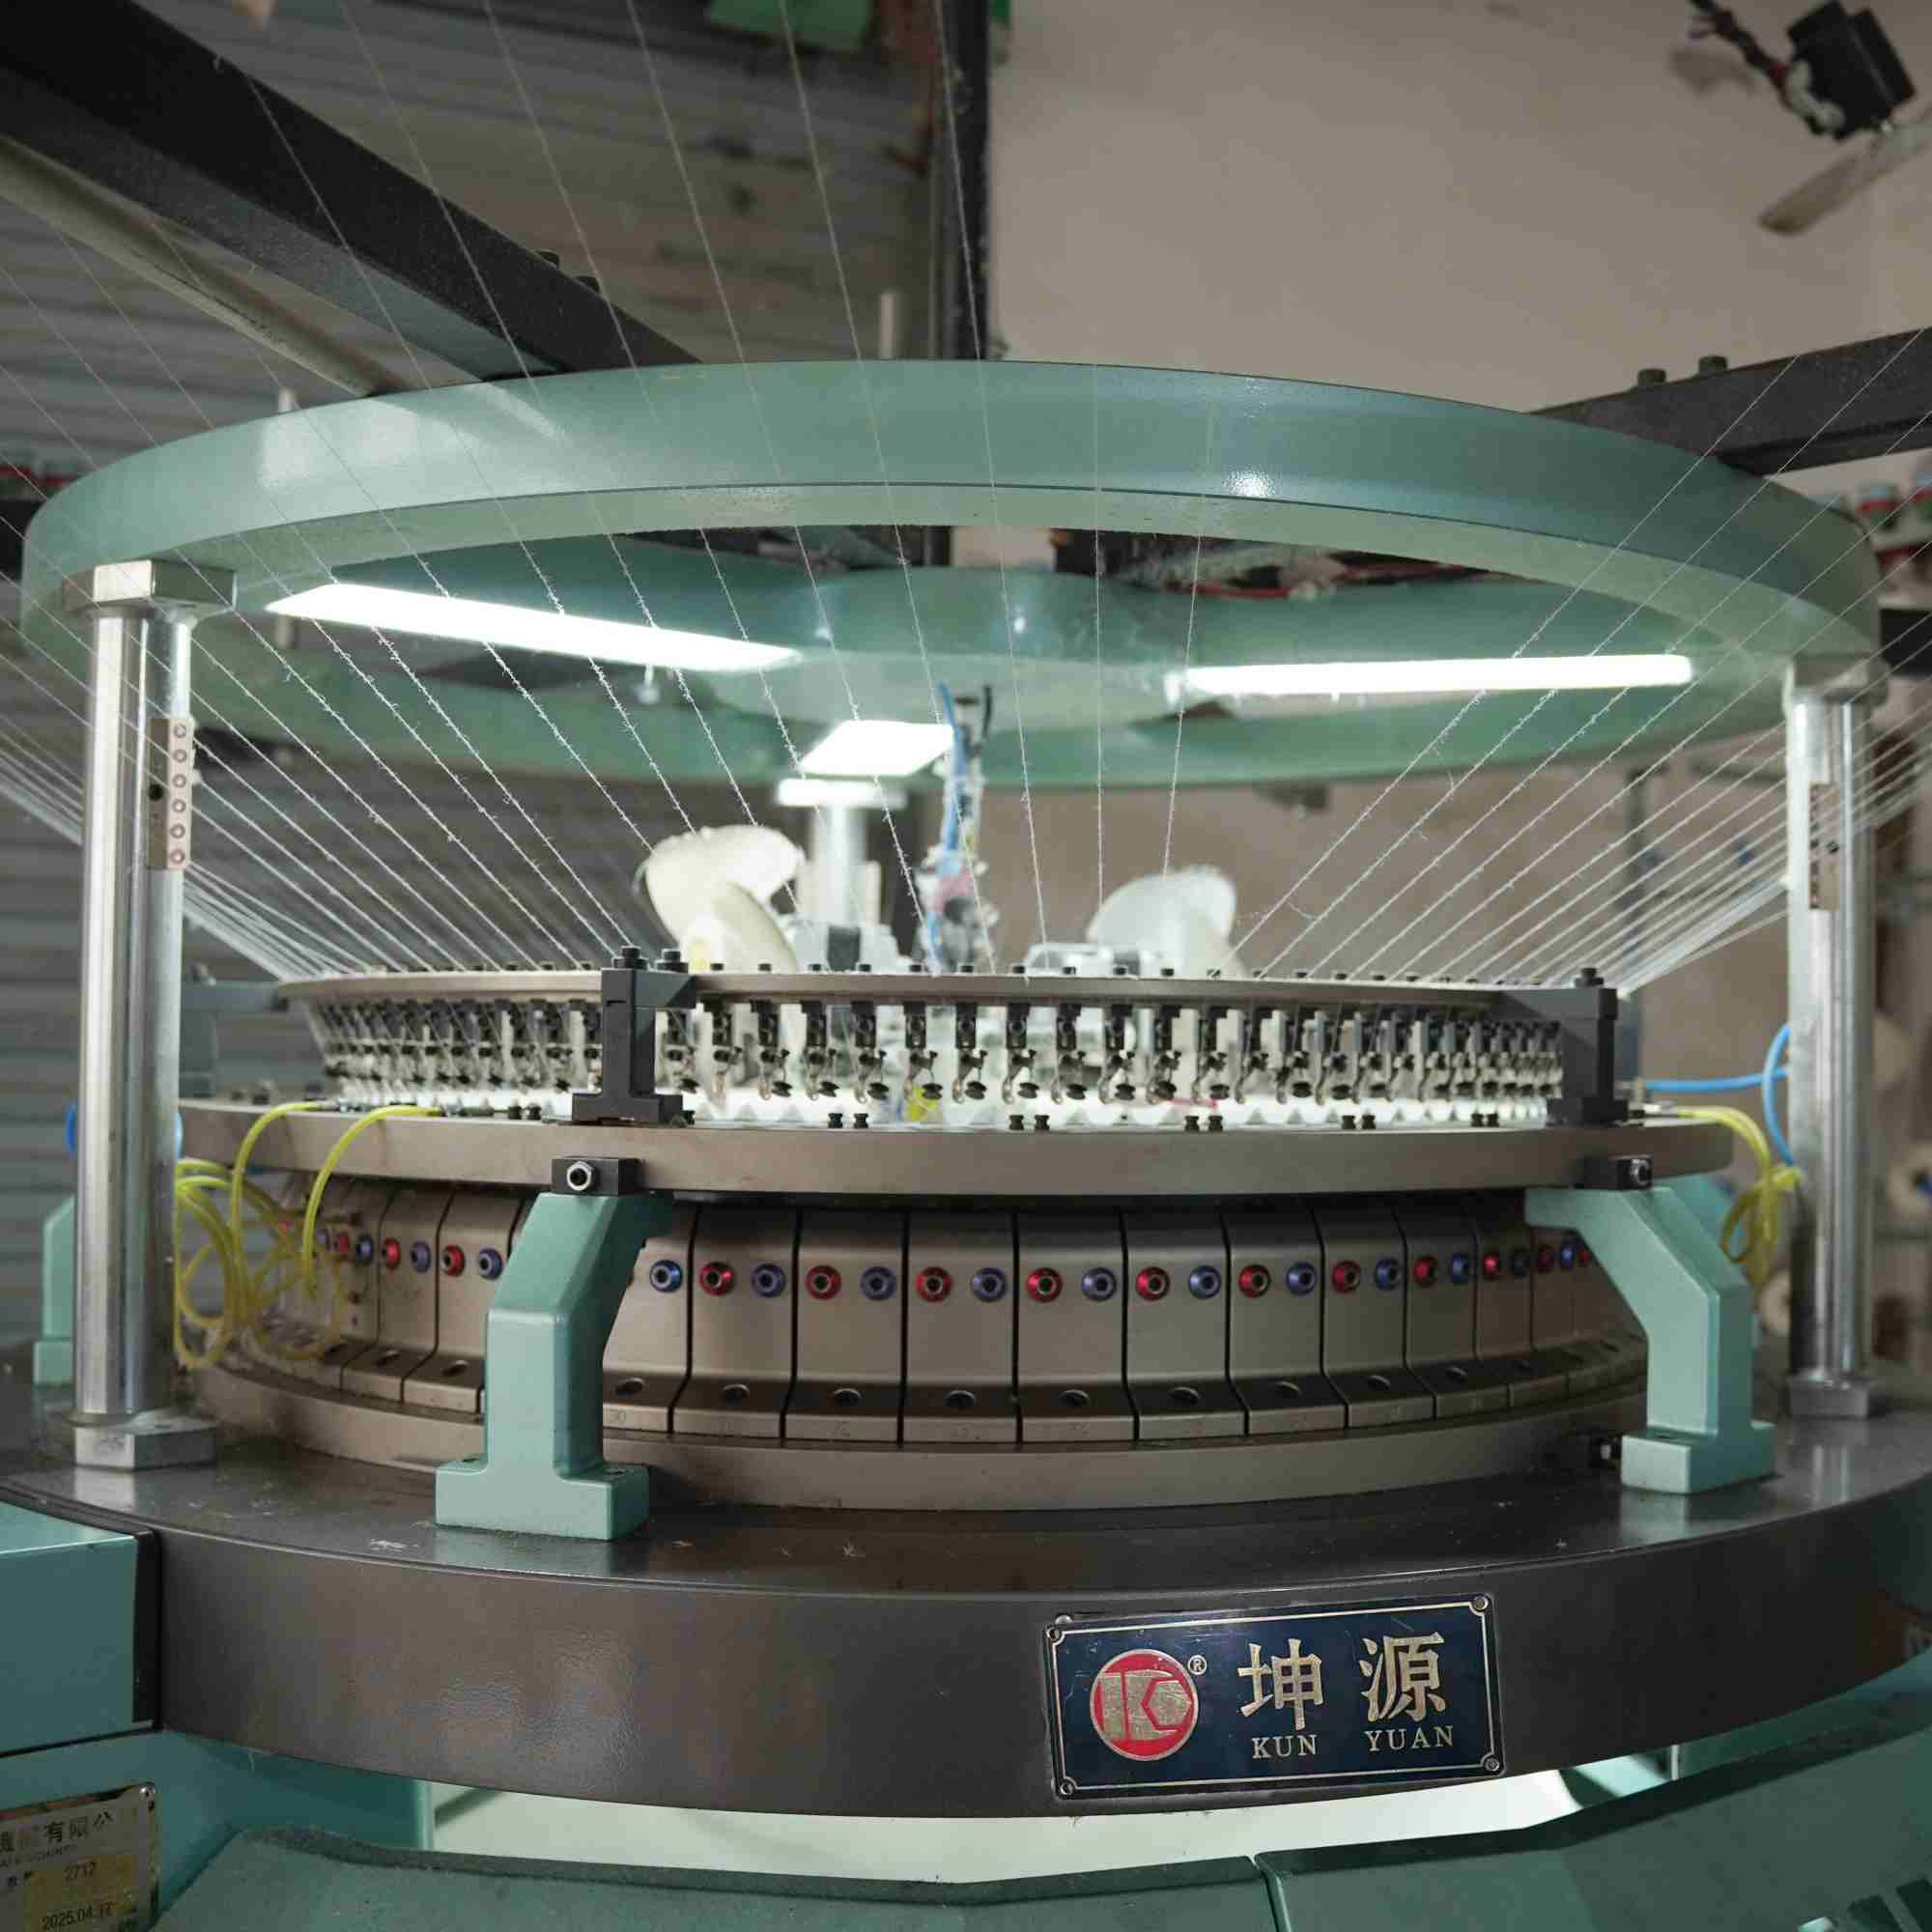
Use the loop calculation only for the specified plain single jersey: one identified ground yarn, actual knitting needles and active feeds, and a documented loop at each counted action. Obtain needle count from the installed cylinder record. Tuck, miss, selective knitting, added yarns and changing consumption require a construction-specific calculation.
For this limited case, N means actual knitting needles, F active feeds, r revolutions per minute, l measured stitch length in millimetres and t resultant yarn tex. The theoretical running rate is R = N x F x r x l x t x 60 / 1,000,000,000 kg per running hour. The 2019 IOSR single-jersey study describes the stitches-to-yarn-length-to-mass chain; this tex expression is a dimensional derivation, not a Kunyuan test result.
First calculate loops per minute as N x F x r. Multiplying by l gives yarn millimetres per minute. Divide by 1,000 for metres, multiply by 60 for an hour, then apply tex grams per 1,000 metres and divide grams by 1,000 for kilograms. The three factors of 1,000 explain the denominator. No sample machine parameters are assumed.
STOLL's yarn-numbering documentation defines tex as grams per 1,000 metres and distinguishes resultant counts for folded yarns. Preserve the actual yarn designation and count system. English cotton count Ne is not tex. Missing stitch length or an ambiguous yarn unit leaves the theoretical estimate unresolved; a convenient online example cannot replace the commercial yarn record.
Open a time record with scheduled start and finish, then identify actual knitting intervals and stops inside it. Record setup, cleaning, package changes and faults separately. Define whether meal breaks or planned shutdowns belong to the scheduled denominator before comparing shifts. A stable-running observation and a complete shift answer different questions.
Define availability A as running hours divided by scheduled hours. For constant documented R, estimated gross mass is R x scheduled hours x A, equivalent to R x running hours. If speed changes, calculate identified running segments separately. Do not use speed already averaged across stopped time and then apply availability again: that deducts the same time twice.
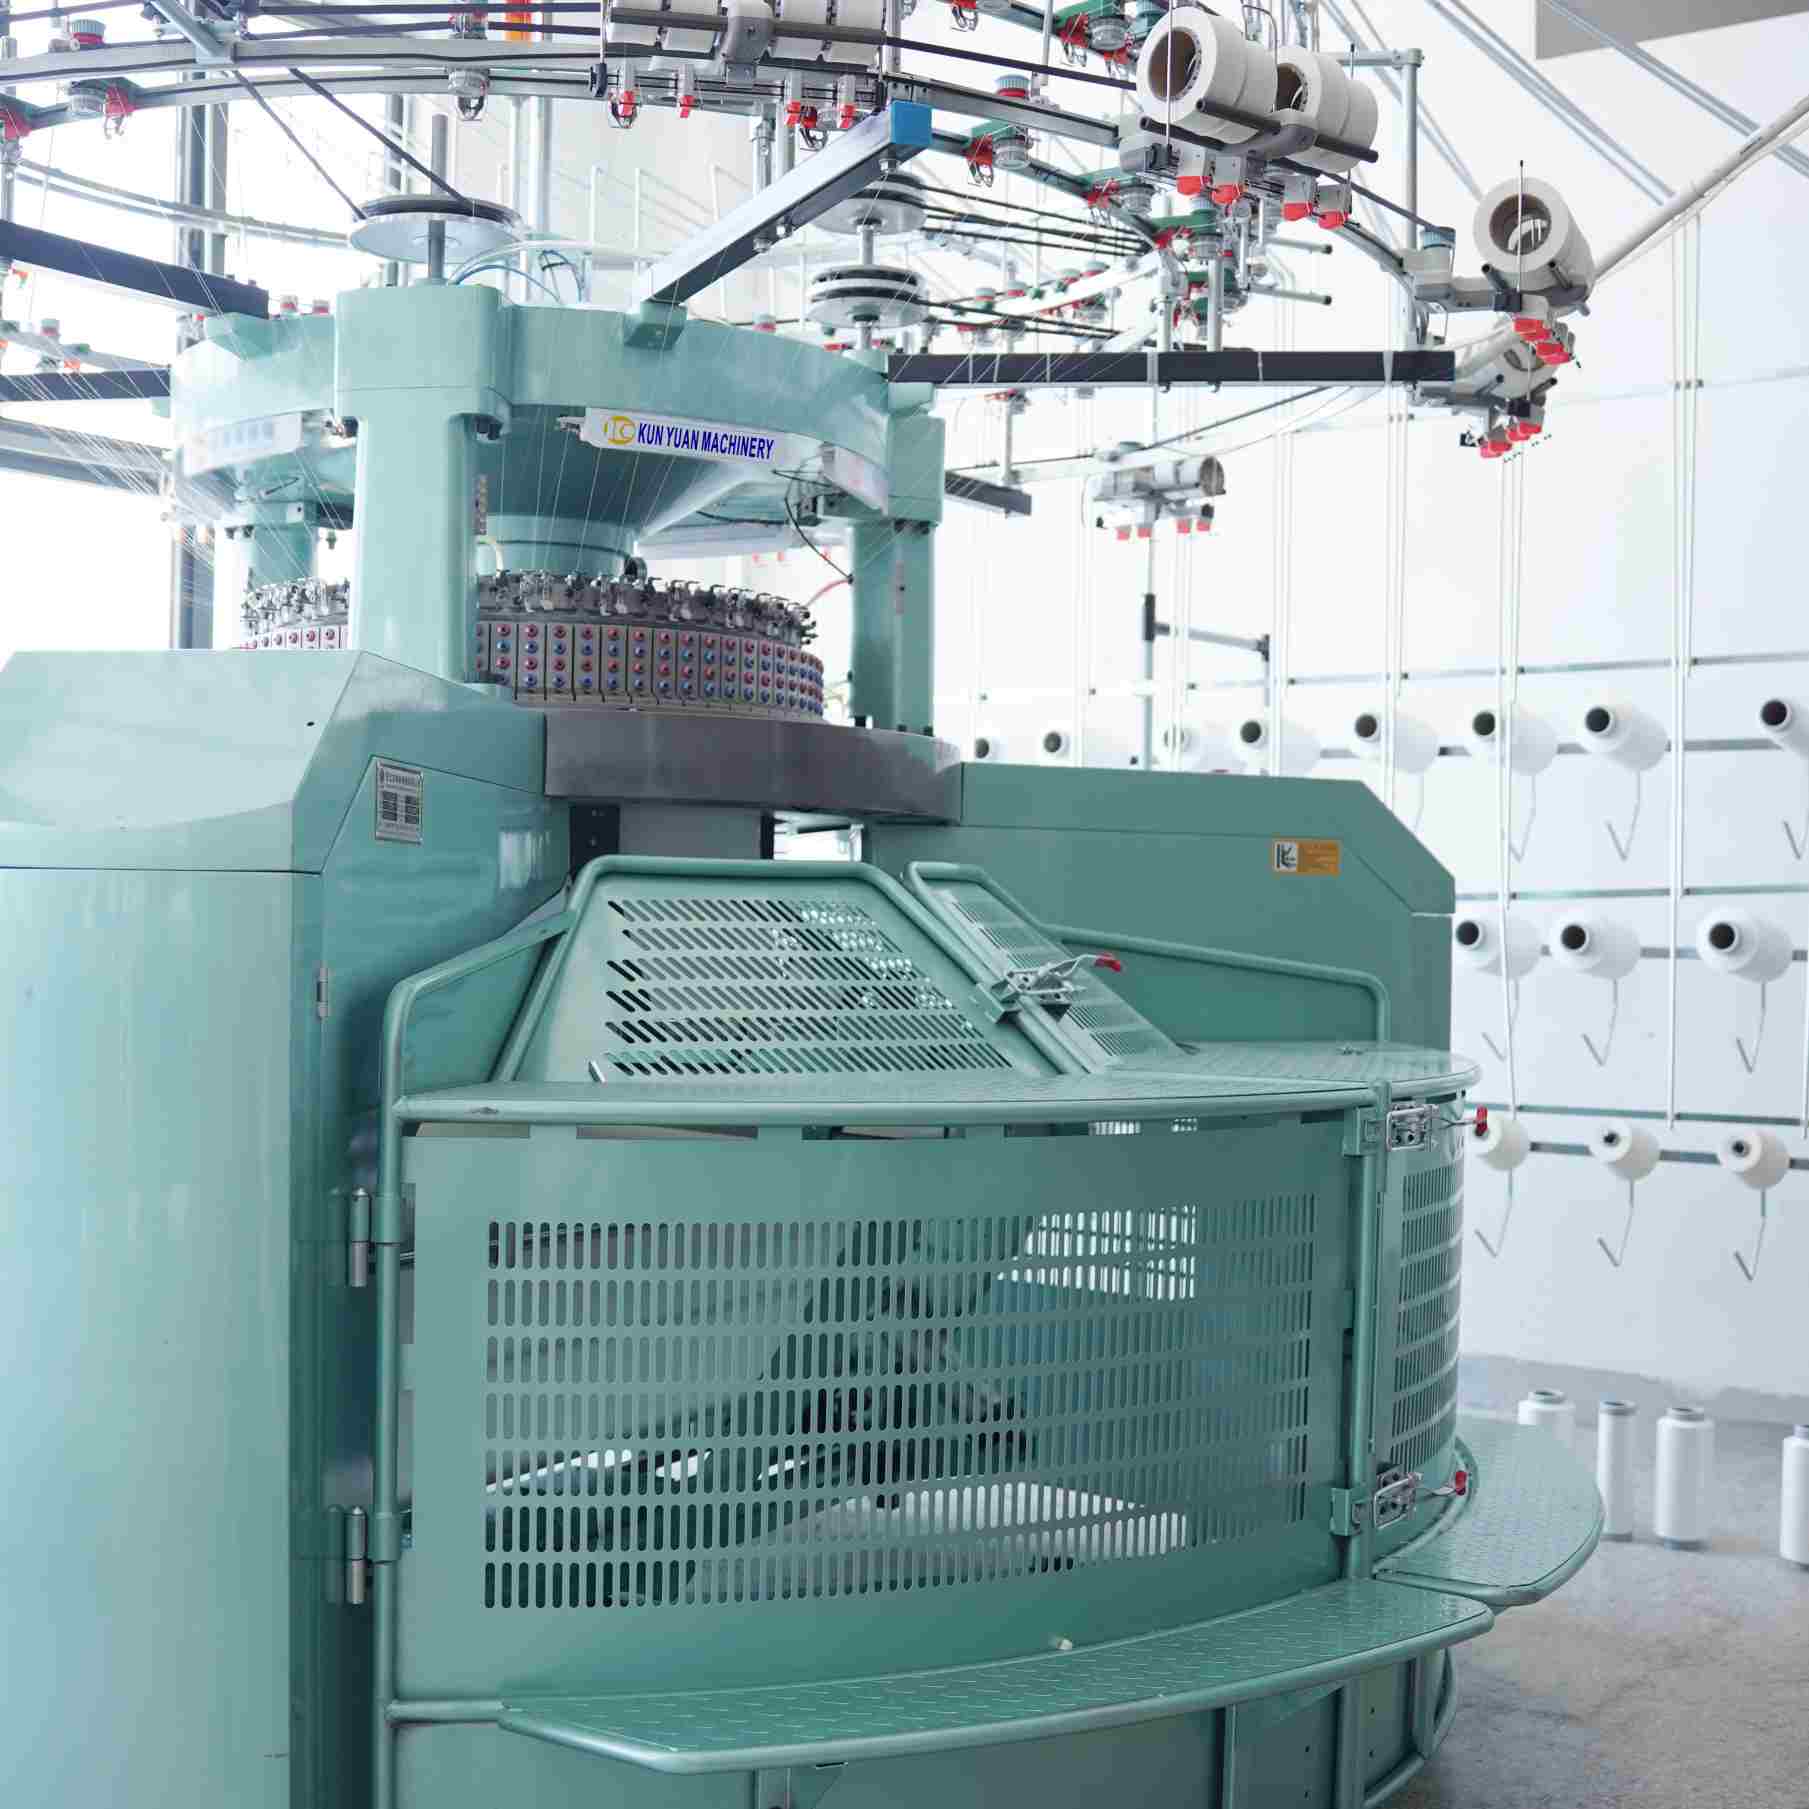
Weigh gross fabric produced in the matched interval using a declared conditioning and tare method. Keep roll identities and settings attached. Investigate differences from the theoretical mass through actual consumption, changed inputs, measurement and material outside the account. Gross knitted mass remains a physical output even when some of it is rejected.
For greige acceptance, classify same-state gross fabric into accepted, trial, held and rejected quantities. Once disposition is complete, quality yield y equals accepted greige mass divided by gross greige mass. The corresponding forecast is R x running hours x y. Finished saleable kilograms require their own linked processing records: fibre removal, moisture or added finishing material can change mass, so finished-to-greige mass is not automatically a pure defect-loss percentage.
| Calculation entry | Unit and definition | Record needed |
|---|---|---|
| Theoretical rate R | kg per running hour for defined plain jersey | N, F, r, l in mm and resultant t in tex |
| Availability A | Running hours / scheduled hours | One interval with all stops classified |
| Greige quality yield y | Accepted greige kg / gross greige kg | Same-state net mass and completed disposition |
| Achieved scheduled rate | Accepted kg / scheduled hours | Attributed rolls, declared endpoint and time basis |
Assign losses once. A yarn break may create both stopped minutes and rejected fabric; those are distinct consequences. Stopped minutes already reduce running hours, while rejected kilograms reduce quality yield. Do not deduct rejected mass again after multiplying by a yield that already excludes it. Held fabric stays pending until its quality decision is complete.
Identify startup and changeover fabric separately from steady output. State whether development samples belong to the order being planned. When the commercial endpoint is dyed or otherwise finished fabric, retain the roll-to-processing-batch link and the final acceptance state. A clean greige interval cannot complete a downstream decision that has not yet been measured.
Test the calculation against a record containing machine identity, construction, yarn lot, measured loop length, active feeds, observed running speed, timestamps, gross mass and disposition. Kunyuan's single-jersey product guidance requests yarn-specific trials and records of speed, stops, width, weight and finishing. It does not guarantee a kilograms-per-hour result for every configuration.
Report stable-trial kg per running hour separately from order or shift kg per scheduled hour. Repeat the relevant route before using a short demonstration for delivery planning. Preserve unexplained differences and pending finishing results. Compare the stated formula, actual inputs and measured accepted output rather than treating one favourable interval as an annual capacity promise.

Use the installed needle count where available. Diameter and gauge can orient an estimate only under the stated builder convention and full-needle assumption. They do not establish the actual active count, feeds or yarn consumption of the construction being evaluated.
A higher running speed increases the simple theoretical rate only while the other inputs remain fixed. Compare actual running time, fabric defects and accepted output before deciding whether the order gains capacity. Do not insert a universal efficiency percentage to force a desired result.
For fabric in one defined state, a mass cross-check is measured area in square metres x measured GSM / 1,000, giving kilograms. Establish the real open area of tubular fabric rather than treating laid-flat width as its entire surface. This geometric check does not convert greige dimensions into finished delivery metres.
Keep the estimate pending when units, time attribution or disposition remain unresolved. An hourly rate with no elapsed time is undefined. A positive scheduled interval with no accepted output has zero accepted output for that interval; report the failure or hold instead of presenting theoretical capacity as achieved production.
Bring the yarn identity, construction, measured loop length and time-and-roll ledger to Kunyuan. Request an observed single-jersey trial reporting theoretical running output, actual gross fabric and accepted output on separately named time bases. Leave missing inputs open until the proposed build and buyer yarn supply the evidence.
Explore the single jersey machine range
 Tel: +86-13859034518
 Email: info@kunyuanmachine.com
 MP/WhatsApp: +86-13859034518
 Manufacturer Address:Bacuo Village, Yonghe Town, Jinjiang City, Fujian Province