Choose open width by the downstream fabric route, not by the frame label
Open-width handling changes the path after loop formation. The buyer must decide where the tube is slit, how the single layer is spread and wound, and whether edge, crease and cross-width quality remain acceptable through finishing.
Start with the final product and process. Define technical face, finished usable width, weight, surface sensitivity, center-crease limit, edge allowance, inspection method, dyeing or finishing route and roll presentation needed by the next department. Compare that destination with a tubular route. Open width may reduce one handling problem while creating a cut edge, slitting waste and additional alignment duties.
Terrot publishes specific machines and frames with open-width arrangements and distinguishes them from tubular and industrial frames. Those pages establish that open width is a named equipment configuration, not a universal accessory for every model or diameter. The quotation must identify the knitting head, compatible frame, slitting and spread path, take-down and winding package for one offered build. Commercial release depends on a full roll accepted by the next process.
Stage one: decide whether the product should leave knitting as a single layer
Map the route from greige knitting to final cutting or conversion. Record whether the downstream process needs immediate face inspection, flat spreading, a wide finishing path or avoidance of a tubular center fold. Note surfaces that mark under pressure, patterns that must remain registered and products whose usable width depends on controlled opening. A downstream preference is not enough; it should be linked to measurable quality or handling gain.
Build a comparable tubular route beside it. Include later slitting, extra unfolding, crease recovery, roll handling, edge trimming and operator work. State where each route creates waste or quality holds. The decision is product-specific: one mill may benefit from an open-width roll for a sensitive finish while another may preserve a tube until a controlled downstream opening stage.
Link the compatible frame to one downstream product route.
Stage two: place the slit on a controlled fabric coordinate
Define the intended slit line relative to machine direction, fabric structure, pattern repeat and any acceptable edge allowance. Identify how the compatible frame guides the tube to the cutting position and how detection or operator checks are performed under the exact manufacturer procedure. Do not publish blade settings or generic alignment values. The delivered manual and qualified roles govern setup, guarding and maintenance.
Mark start-up, any slit correction, stop, restart and roll change. Inspect for wandering cuts, damaged adjacent loops, lost pattern width, contamination and edge curl. Preserve samples around every transition. If the fabric has a repeat or engineered zone, demonstrate that the cut line does not migrate into saleable content over a representative run.
Mark slit corrections and inspect both edges through the roll.
Stage three: stabilize spreading, take-down and winding as one handling system
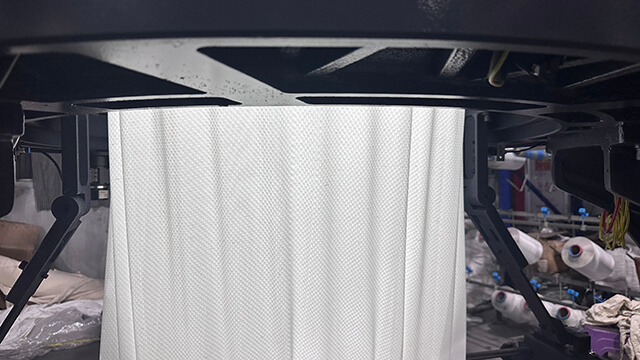
Observe how the cut fabric opens from tube to single layer and enters take-down and winding. Record technical-face orientation, edge tracking, cross-width tension evidence, roll hardness or pressure method supported by the equipment, and any fold, bow, skew or surface mark. A clean knitting head can still deliver an unusable roll if spreading and winding distort the fabric.
Inspect the beginning, middle and end of the roll across its width. Compare left edge, center and right edge for width, appearance and local stretch using the buyer's method. Include a planned stop and restart and an ordinary roll change. Keep adjustments controlled and marked. The accepted handling window should not depend on an unrecorded operator correction.
Use downstream accepted width and loss to close the process.
Stage four: let finishing and cutting approve the full open-width roll
Send an identified roll or representative full-width sections through the actual relaxation, dyeing, heat or coating route. Recheck usable width, edge loss, center appearance, bow or skew, dimensional response, surface and pattern alignment. Record whether the next process needs re-spreading, edge trimming or repair. Those losses belong in the route comparison rather than disappearing after knitting acceptance.
Reconcile gross roll weight or length, slit and edge waste, held regions, finishing loss and accepted downstream quantity. Ask the receiving department to sign the roll disposition and report handling problems by coordinate. Release the route after a repeated roll meets the same criteria following a normal style or setup change.
Open-width process release table
Process stage
Control record
Fabric evidence
Hold condition
Route choice
Product and next-process roll form
Tubular versus open-width comparison
Benefit is undefined
Slitting
Coordinate, edge allowance and events
Marked cut-edge samples
Line or damage drifts
Spreading and winding
Orientation, width and roll positions
Cross-width inspection
Edge or pressure loss hidden
Downstream release
Finish, losses and receiving feedback
Accepted repeated roll
Only machine-side quality passes
Open-width circular knitting questions
Does an open-width frame eliminate every center mark?
No. The exact fabric, spreading, winding and downstream route must demonstrate the required appearance.
Can an open-width system be added to any circular machine?
Do not assume so. Confirm compatibility, frame, slitting, take-down and control scope for the exact model.
What evidence should be kept around the slit?
Retain the line coordinate, edge allowance, event marks and samples before and after any correction.
Why inspect across the full width?
Edge curl, skew, tension differences and pressure marks may be hidden by a center-only sample or average width.
Who closes open-width acceptance?
The next process should accept the roll after the intended finish with edge and handling losses included.
05
Conclusion
Open width is a complete material-handling route. Product need opens the decision, a controlled slit creates the single layer, spreading and winding preserve its geometry, and downstream acceptance proves its value. Treating all four stages as one record prevents a crease claim from hiding edge loss, unstable rolls or an incompatible frame.
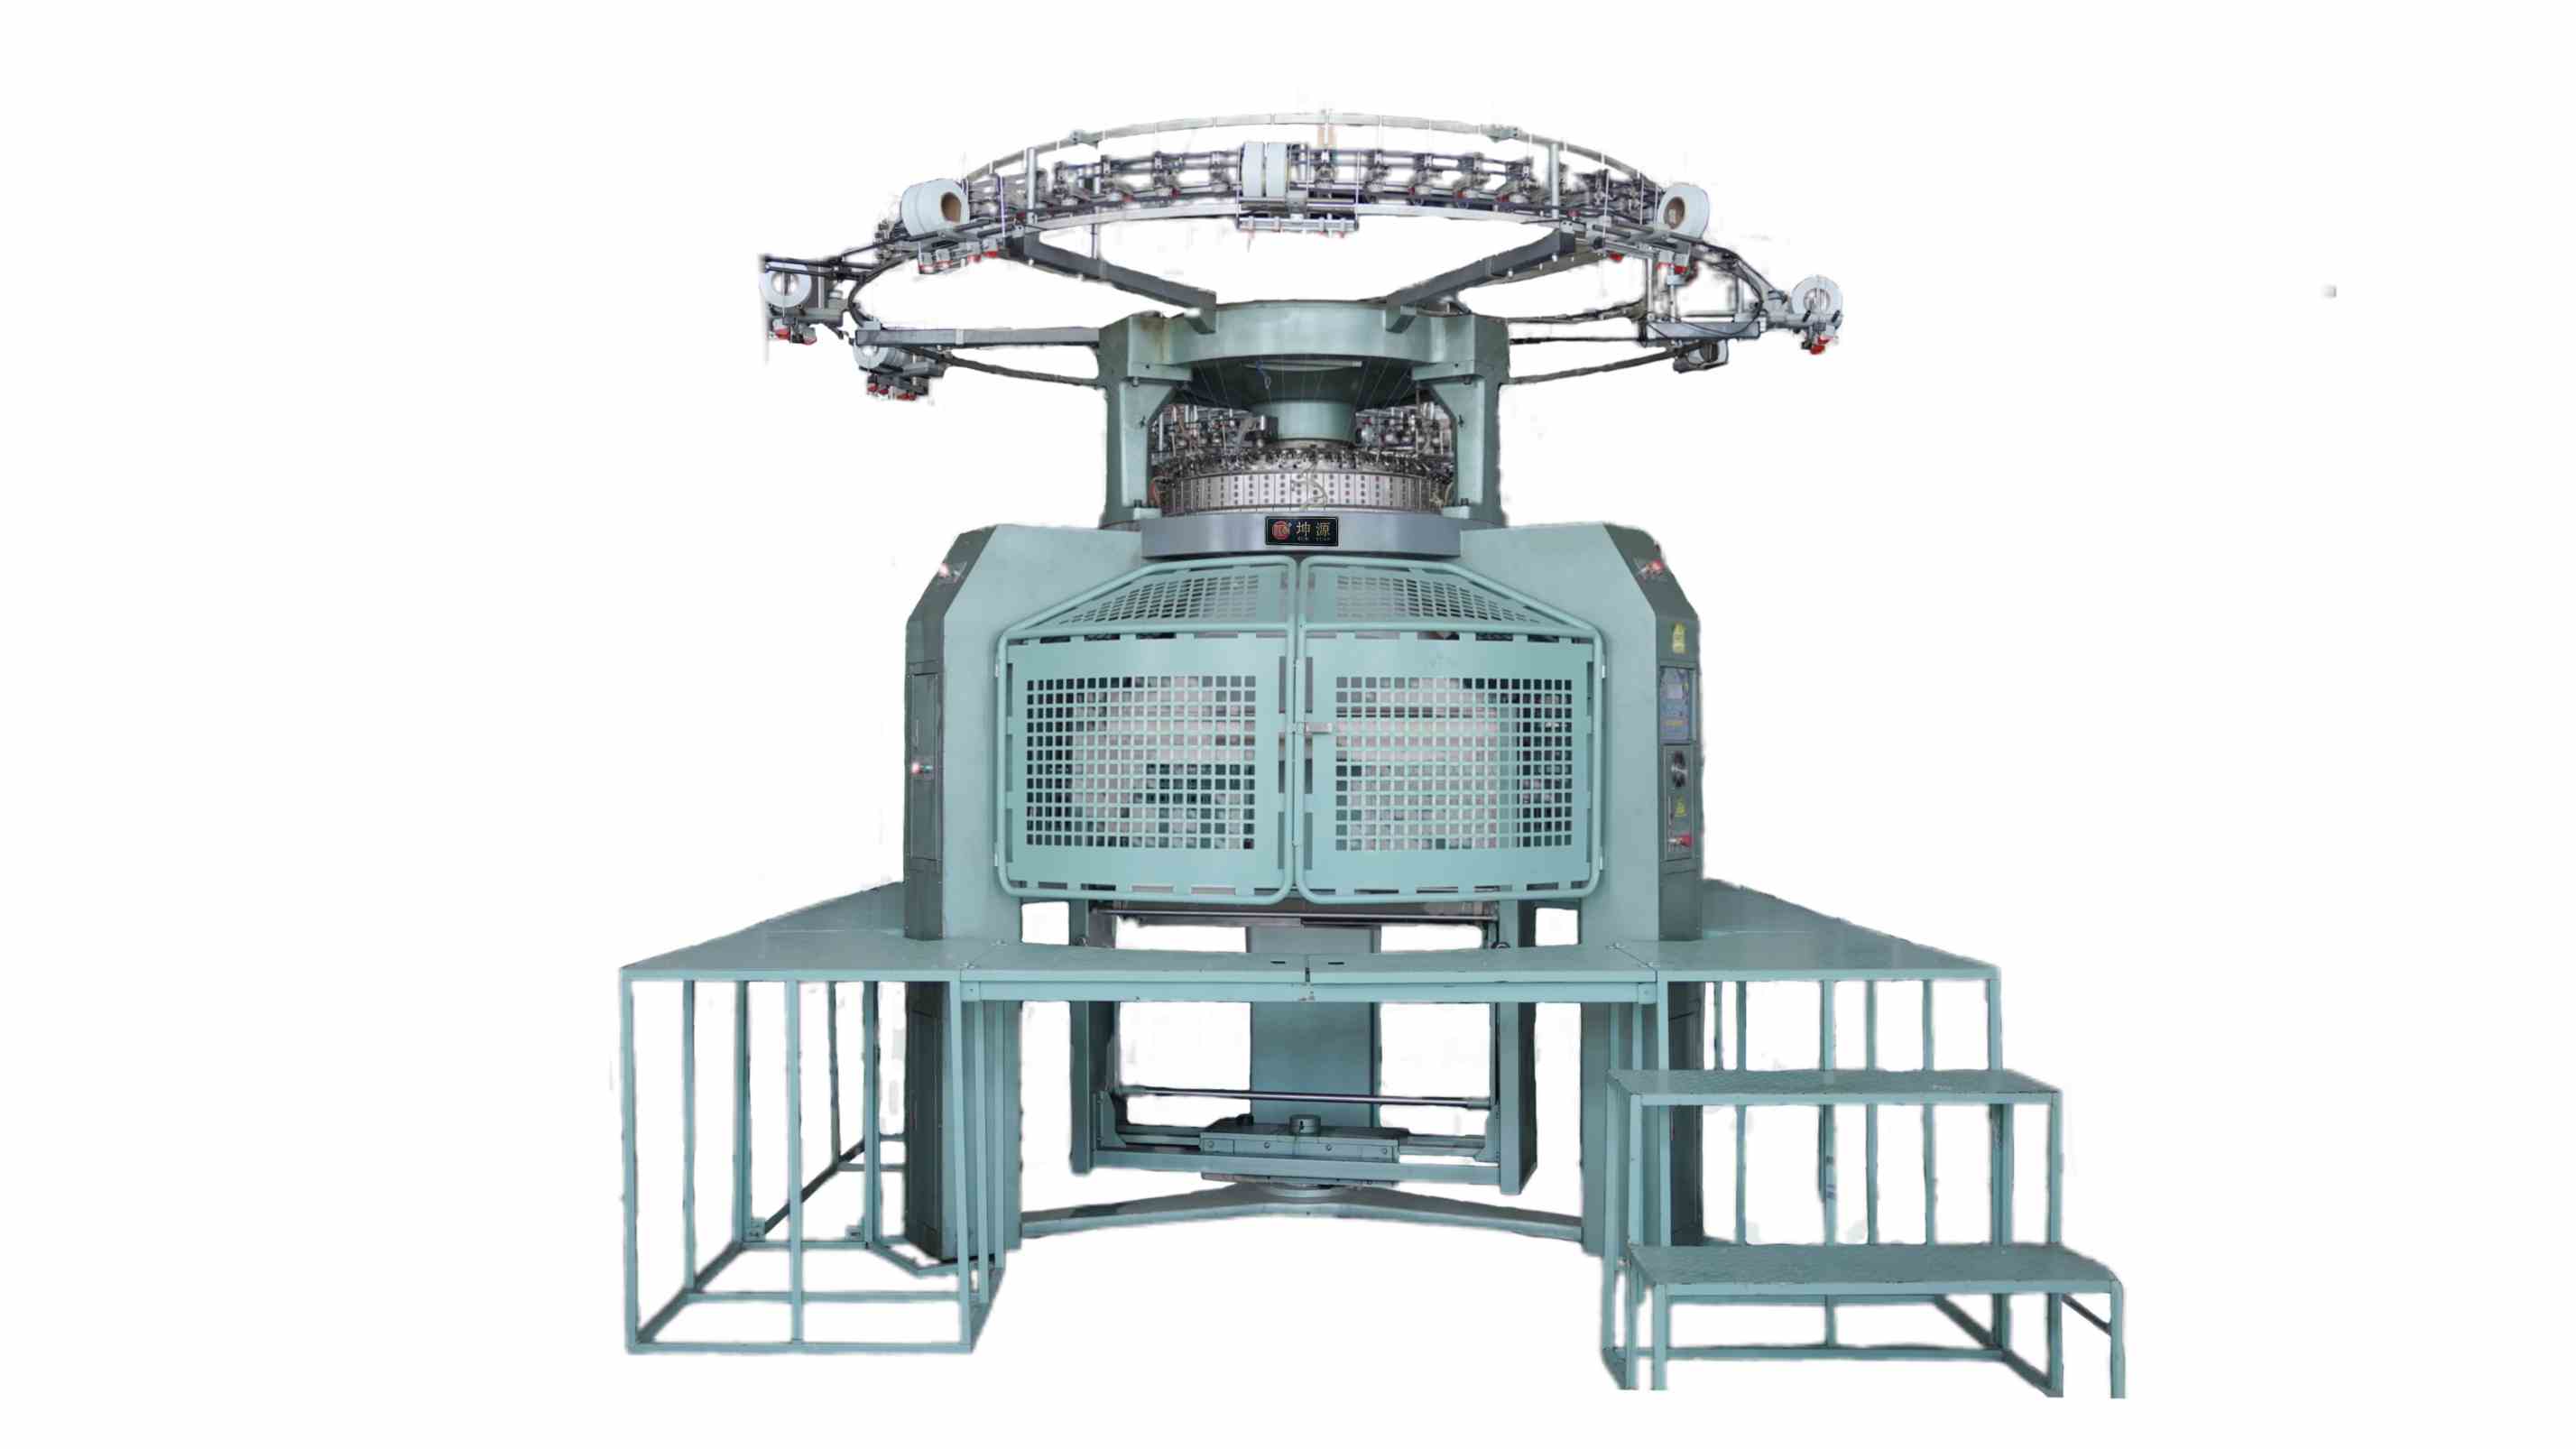
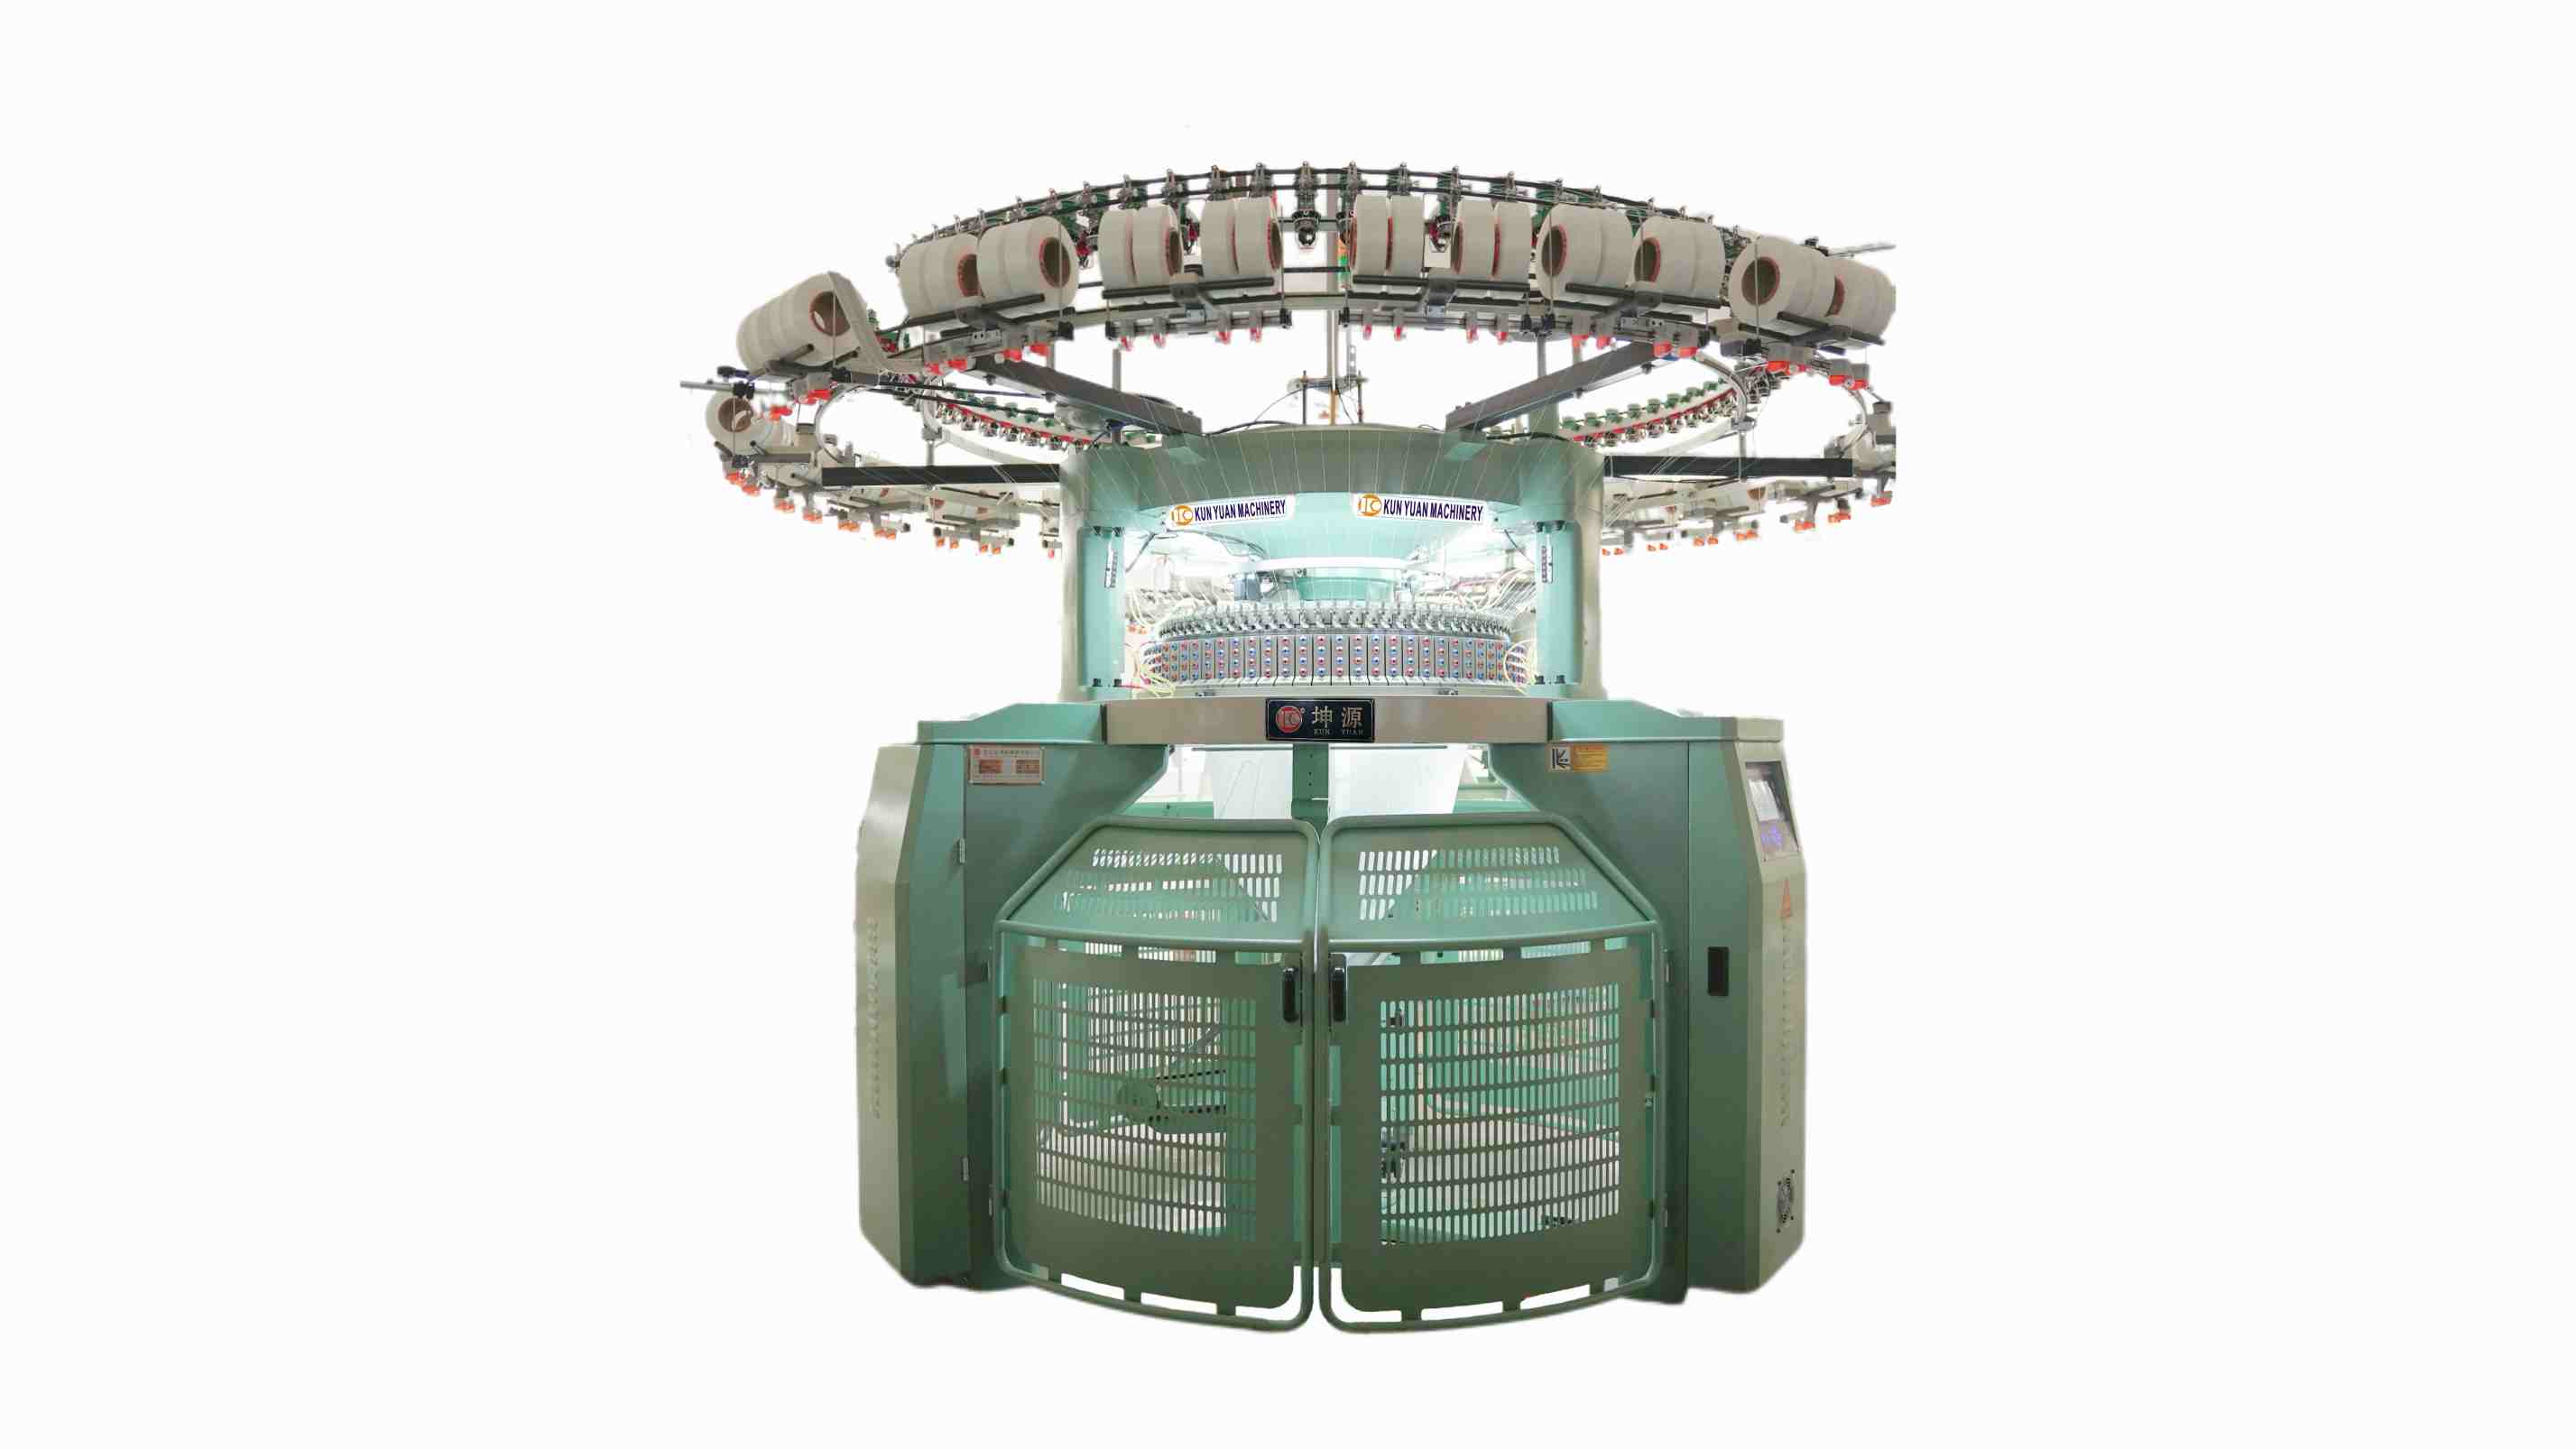
Use this process map when evaluating the open-width circular knitting machine range and require the quoted slitting, spreading and winding system to deliver a downstream-accepted full-width roll.




 Tel: +86-13859034518
 Email: info@kunyuanmachine.com
 MP/WhatsApp: +86-13859034518
 Manufacturer Address:Bacuo Village, Yonghe Town, Jinjiang City, Fujian Province