

Hot Keyword:
Author:KUNYUAN Machine Manufacturer TIME:2026-09-15
A single compressor nameplate or machine catalogue figure cannot size a mill network. Demand changes with installed options, cleaning devices, leaks, pressure stability and how many machines act at the same time.
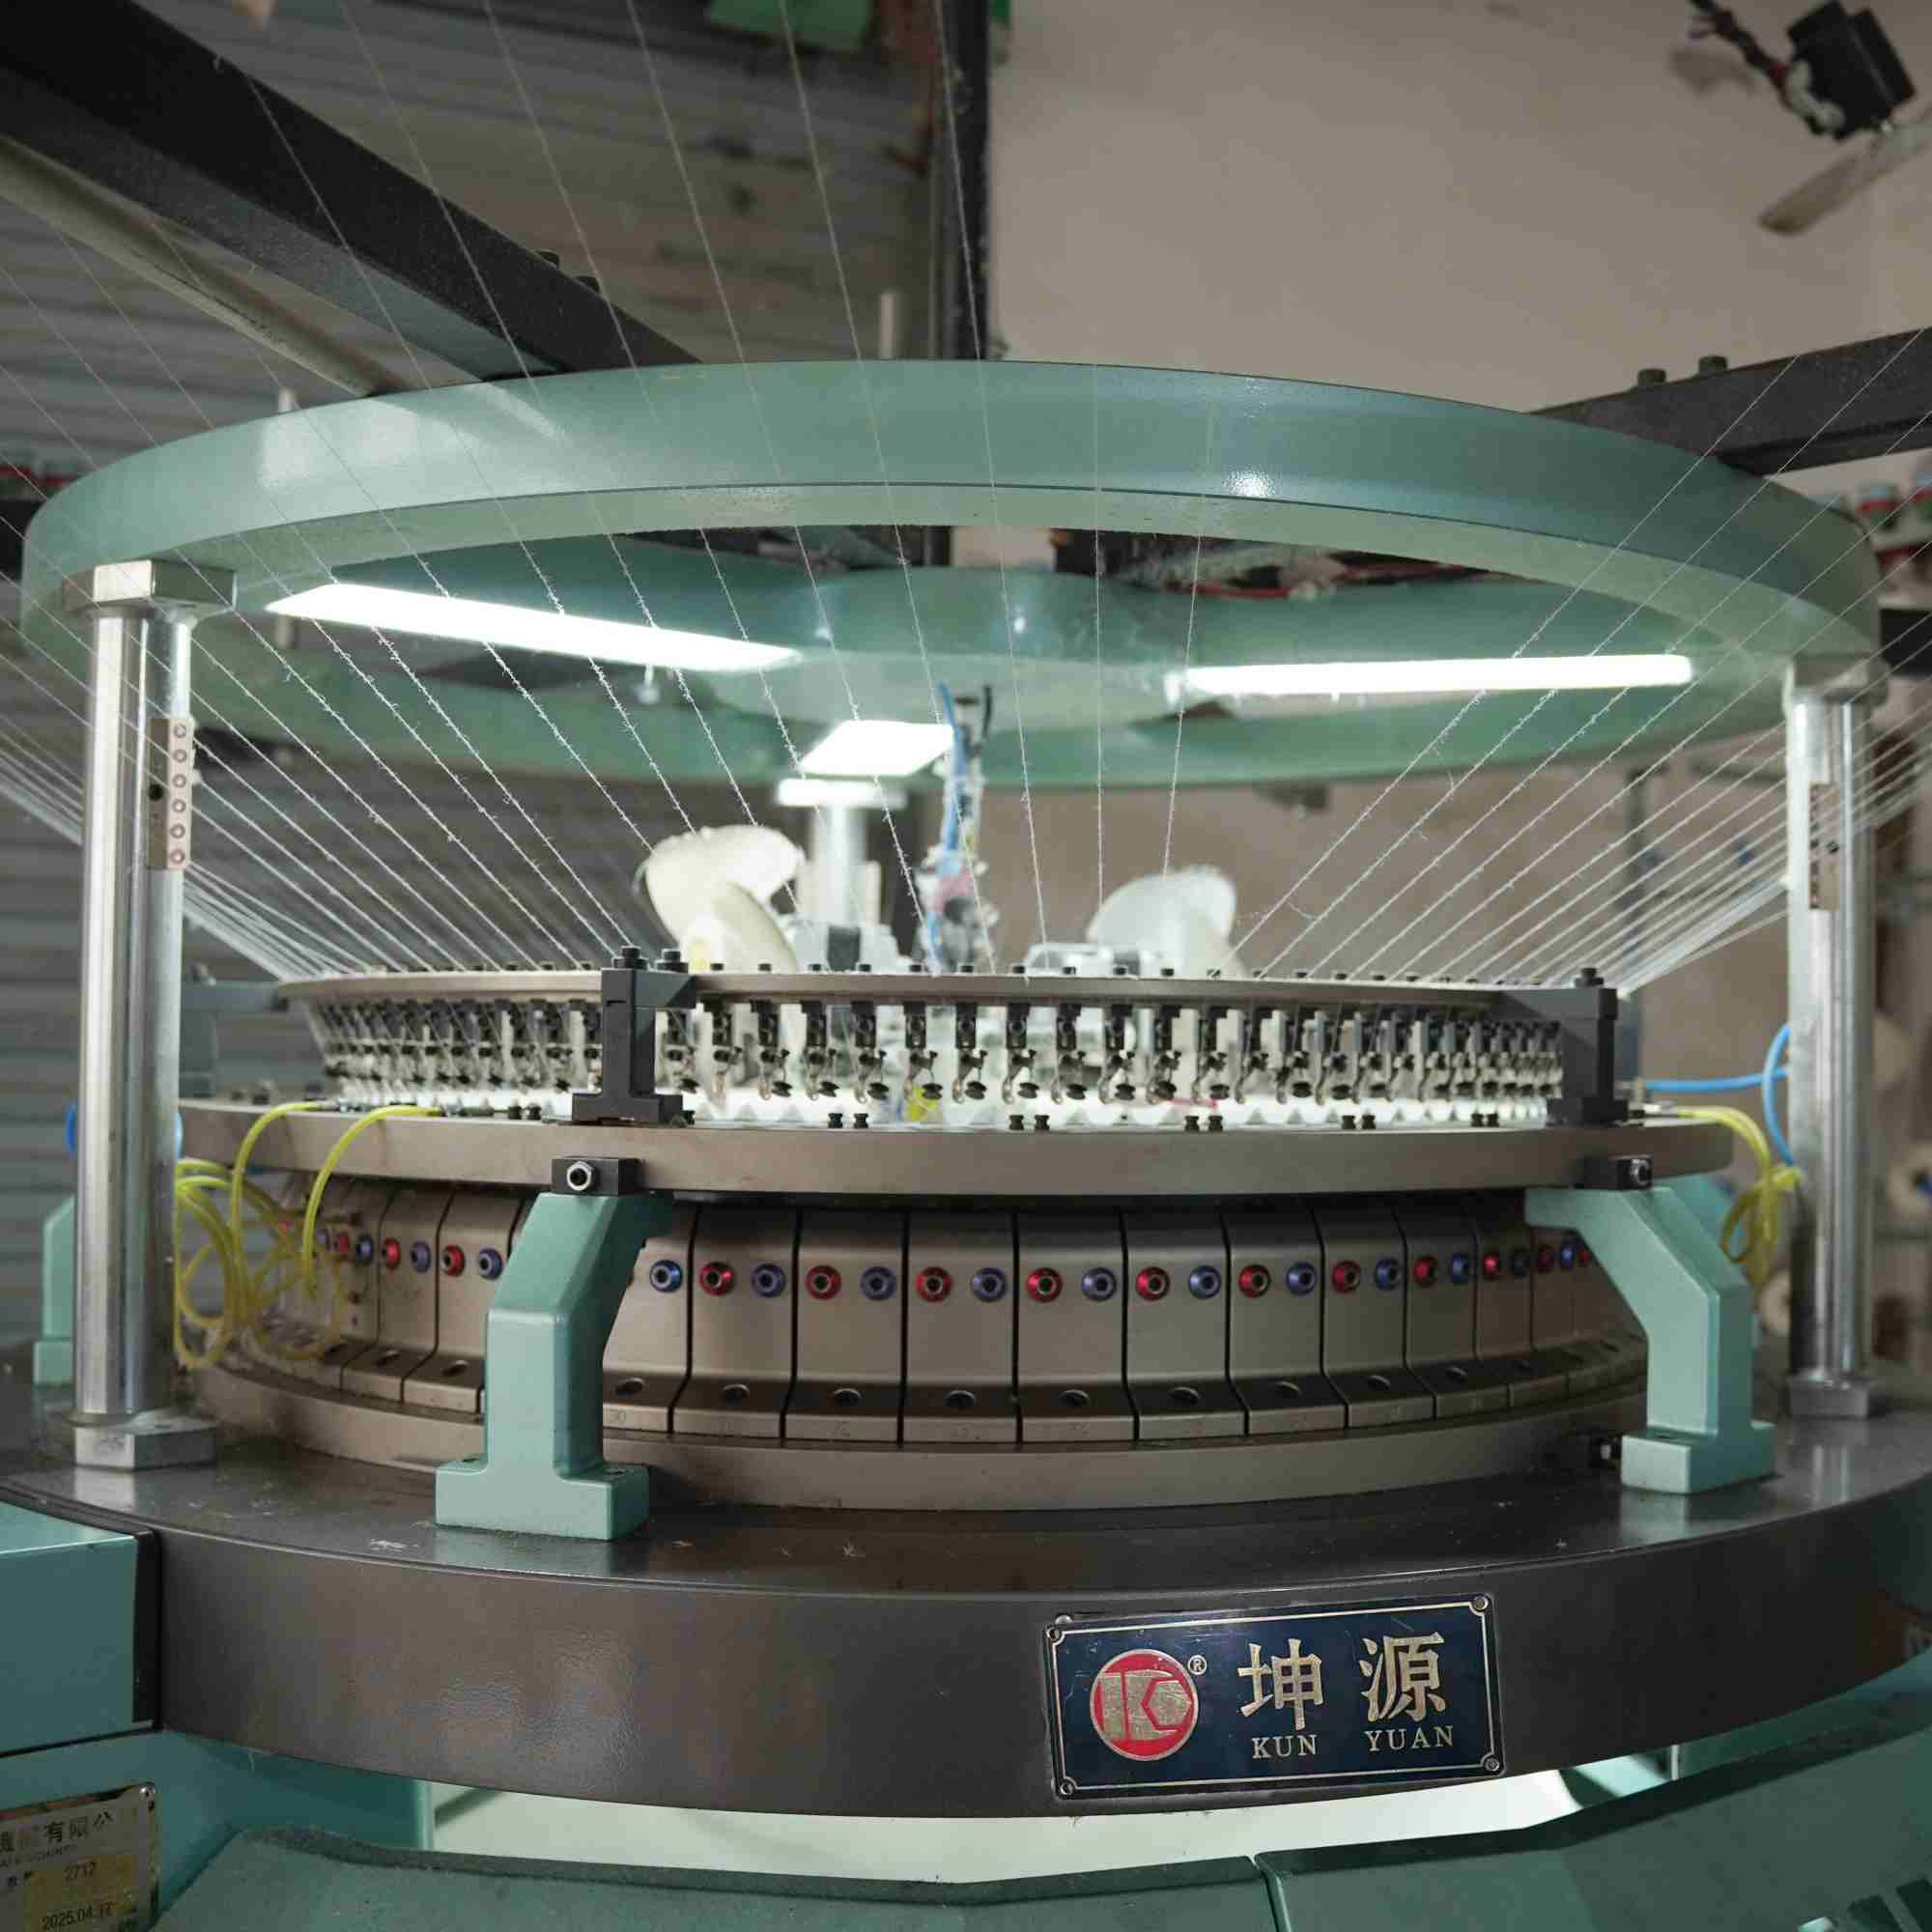
List every pneumatic consumer on the exact offered machine and auxiliary route. Identify the supplier's required pressure and air-quality condition without replacing it with a universal value. Record normal knitting, startup, stop, cleaning or blow-off, style change and idle states separately. Then measure at a defined boundary with calibrated instruments and synchronized timestamps.
Compressed Air Challenge guidance emphasizes the cost and pressure consequences of leaks and the need to understand the complete system. Treat leak load as a separate baseline, not productive machine consumption. For procurement, compare pressure at the machine, measured flow over representative states, concurrency across the line, dryer and filter effects, and accepted fabric output. Qualified utility engineers should perform system sizing and changes.
Walk the machine and approved auxiliaries with supplier documents. Record each air user, whether it is continuous, intermittent or event-driven, its control state and the product styles that activate it. Separate machine functions from handheld cleaning, floor services and other equipment sharing the branch.
Create timestamps for startup, stable knitting, package handling, planned stop, restart, cleaning and idle. An average collected without state labels can hide a short peak that causes pressure loss or a long idle leak that raises energy cost.
| State | Required record | Useful result | Common error |
|---|---|---|---|
| Stable knitting | Flow, pressure, product and time | Productive baseline | No product identity |
| Event peak | Duration and trigger | Storage/pressure review | Treating peak as continuous |
| Idle or stop | Control state and leak load | Nonproductive demand | Charging it to fabric |
| Line schedule | Concurrent machine states | System demand profile | Summing all maxima |
Measure an approved nonproduction condition that reveals branch or machine leakage without defeating controls. Compare with the isolated or supplier-defined state where permitted. Locate audible or instrument-detected leakage through the site's maintenance procedure and record repairs by component and date.
Do not lower pressure or close required supplies simply to improve the number. A repaired leak should be confirmed by the same boundary and state. Keep system pressure stability in view because excessive pressure and pressure drop can both distort demand and machine performance.
Build a time profile for the number of machines expected in each state, including synchronized cleaning or shift events. Add other branch users, distribution losses and treatment equipment through an engineered system model. Avoid multiplying one short peak by every installed machine unless those peaks genuinely coincide.
For efficiency comparison, pair compressed-air energy or measured demand with accepted kilograms for the same product and scheduled period. Include stops and rejected sections. Compressor and storage selection should be completed by qualified system specialists using the verified demand profile and required pressure at the point of use.
No. Verify installed consumers, required pressure, events, leaks, concurrency and the complete distribution system.
Demand and equipment behavior are meaningful only with the pressure and reference conditions identified.
Report it separately as a leak or nonproductive baseline and verify authorized repairs.
Only if the operating schedule shows they occur concurrently.
Pair measured air or energy with accepted fabric for the same product, time window and quality disposition.
Compressed-air sizing begins with states, boundaries and timestamps. Separating productive demand from leaks, then applying realistic concurrency, produces a defensible utility profile. The same ledger prevents an attractive flow number from hiding unstable pressure or low accepted yield and gives engineers the evidence needed to size distribution, storage and compressor capacity responsibly.
Add this utility ledger when comparing the circular knitting machine range and have the final compressed-air system reviewed by qualified engineers against the exact installed options.
 Tel: +86-13859034518
 Email: info@kunyuanmachine.com
 MP/WhatsApp: +86-13859034518
 Manufacturer Address:Bacuo Village, Yonghe Town, Jinjiang City, Fujian Province