Hot Keyword:
YOUR POSITION:HOME > Blog >

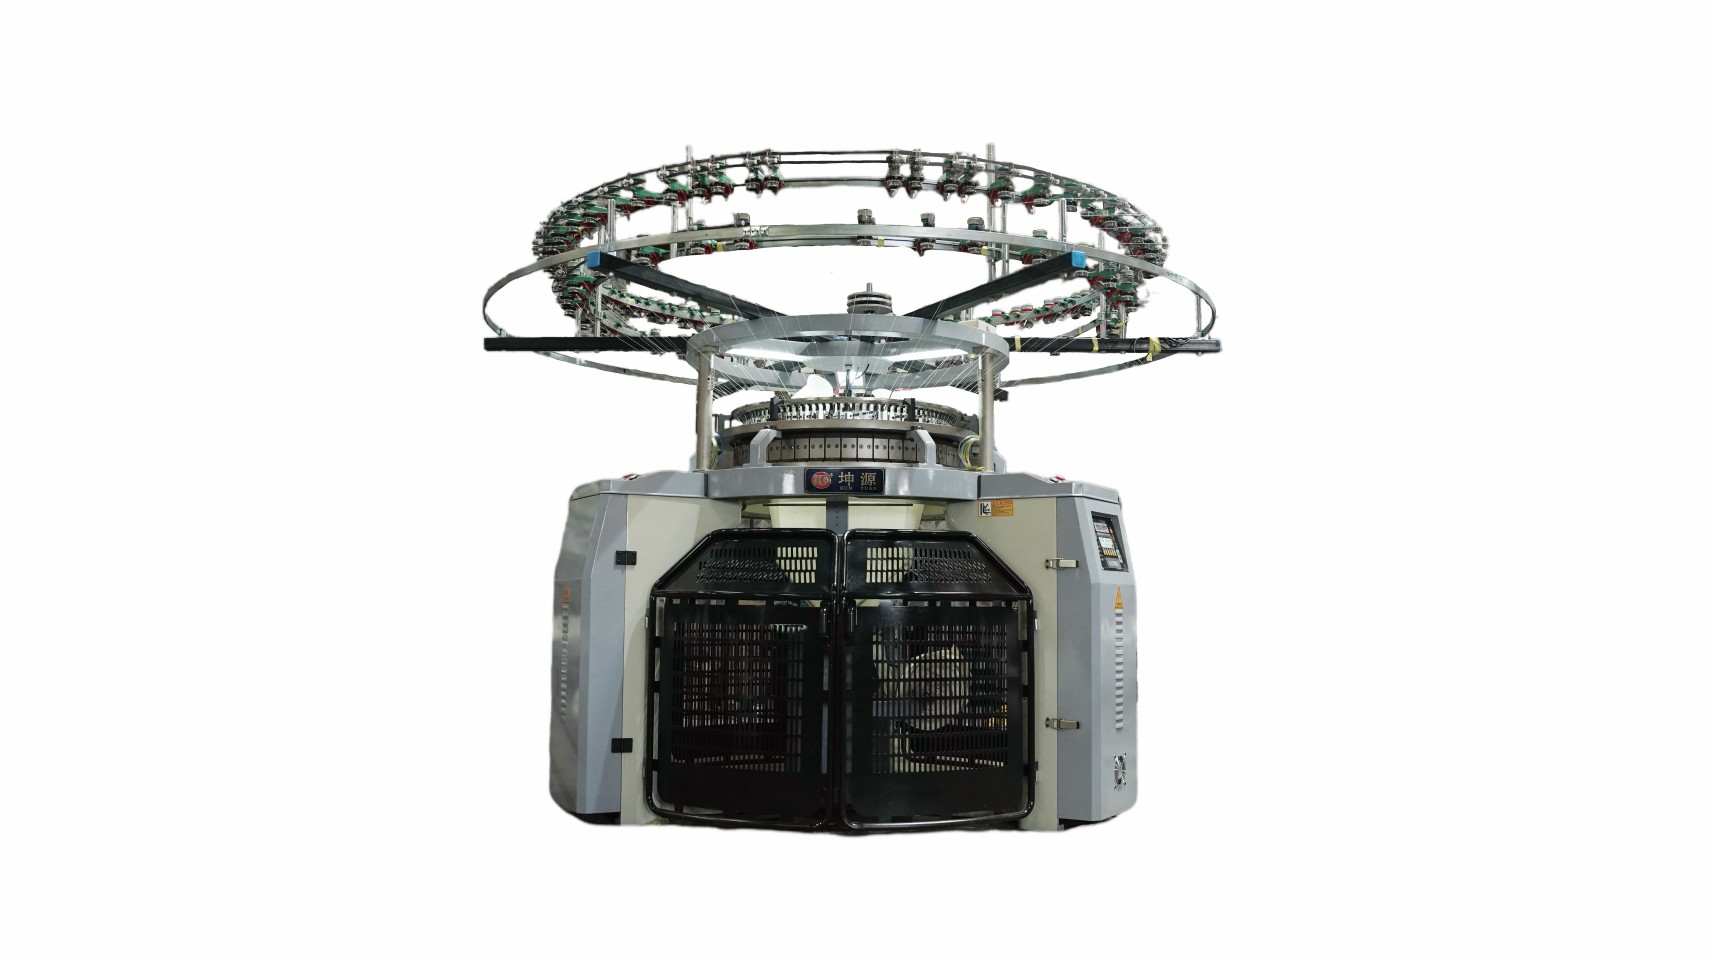
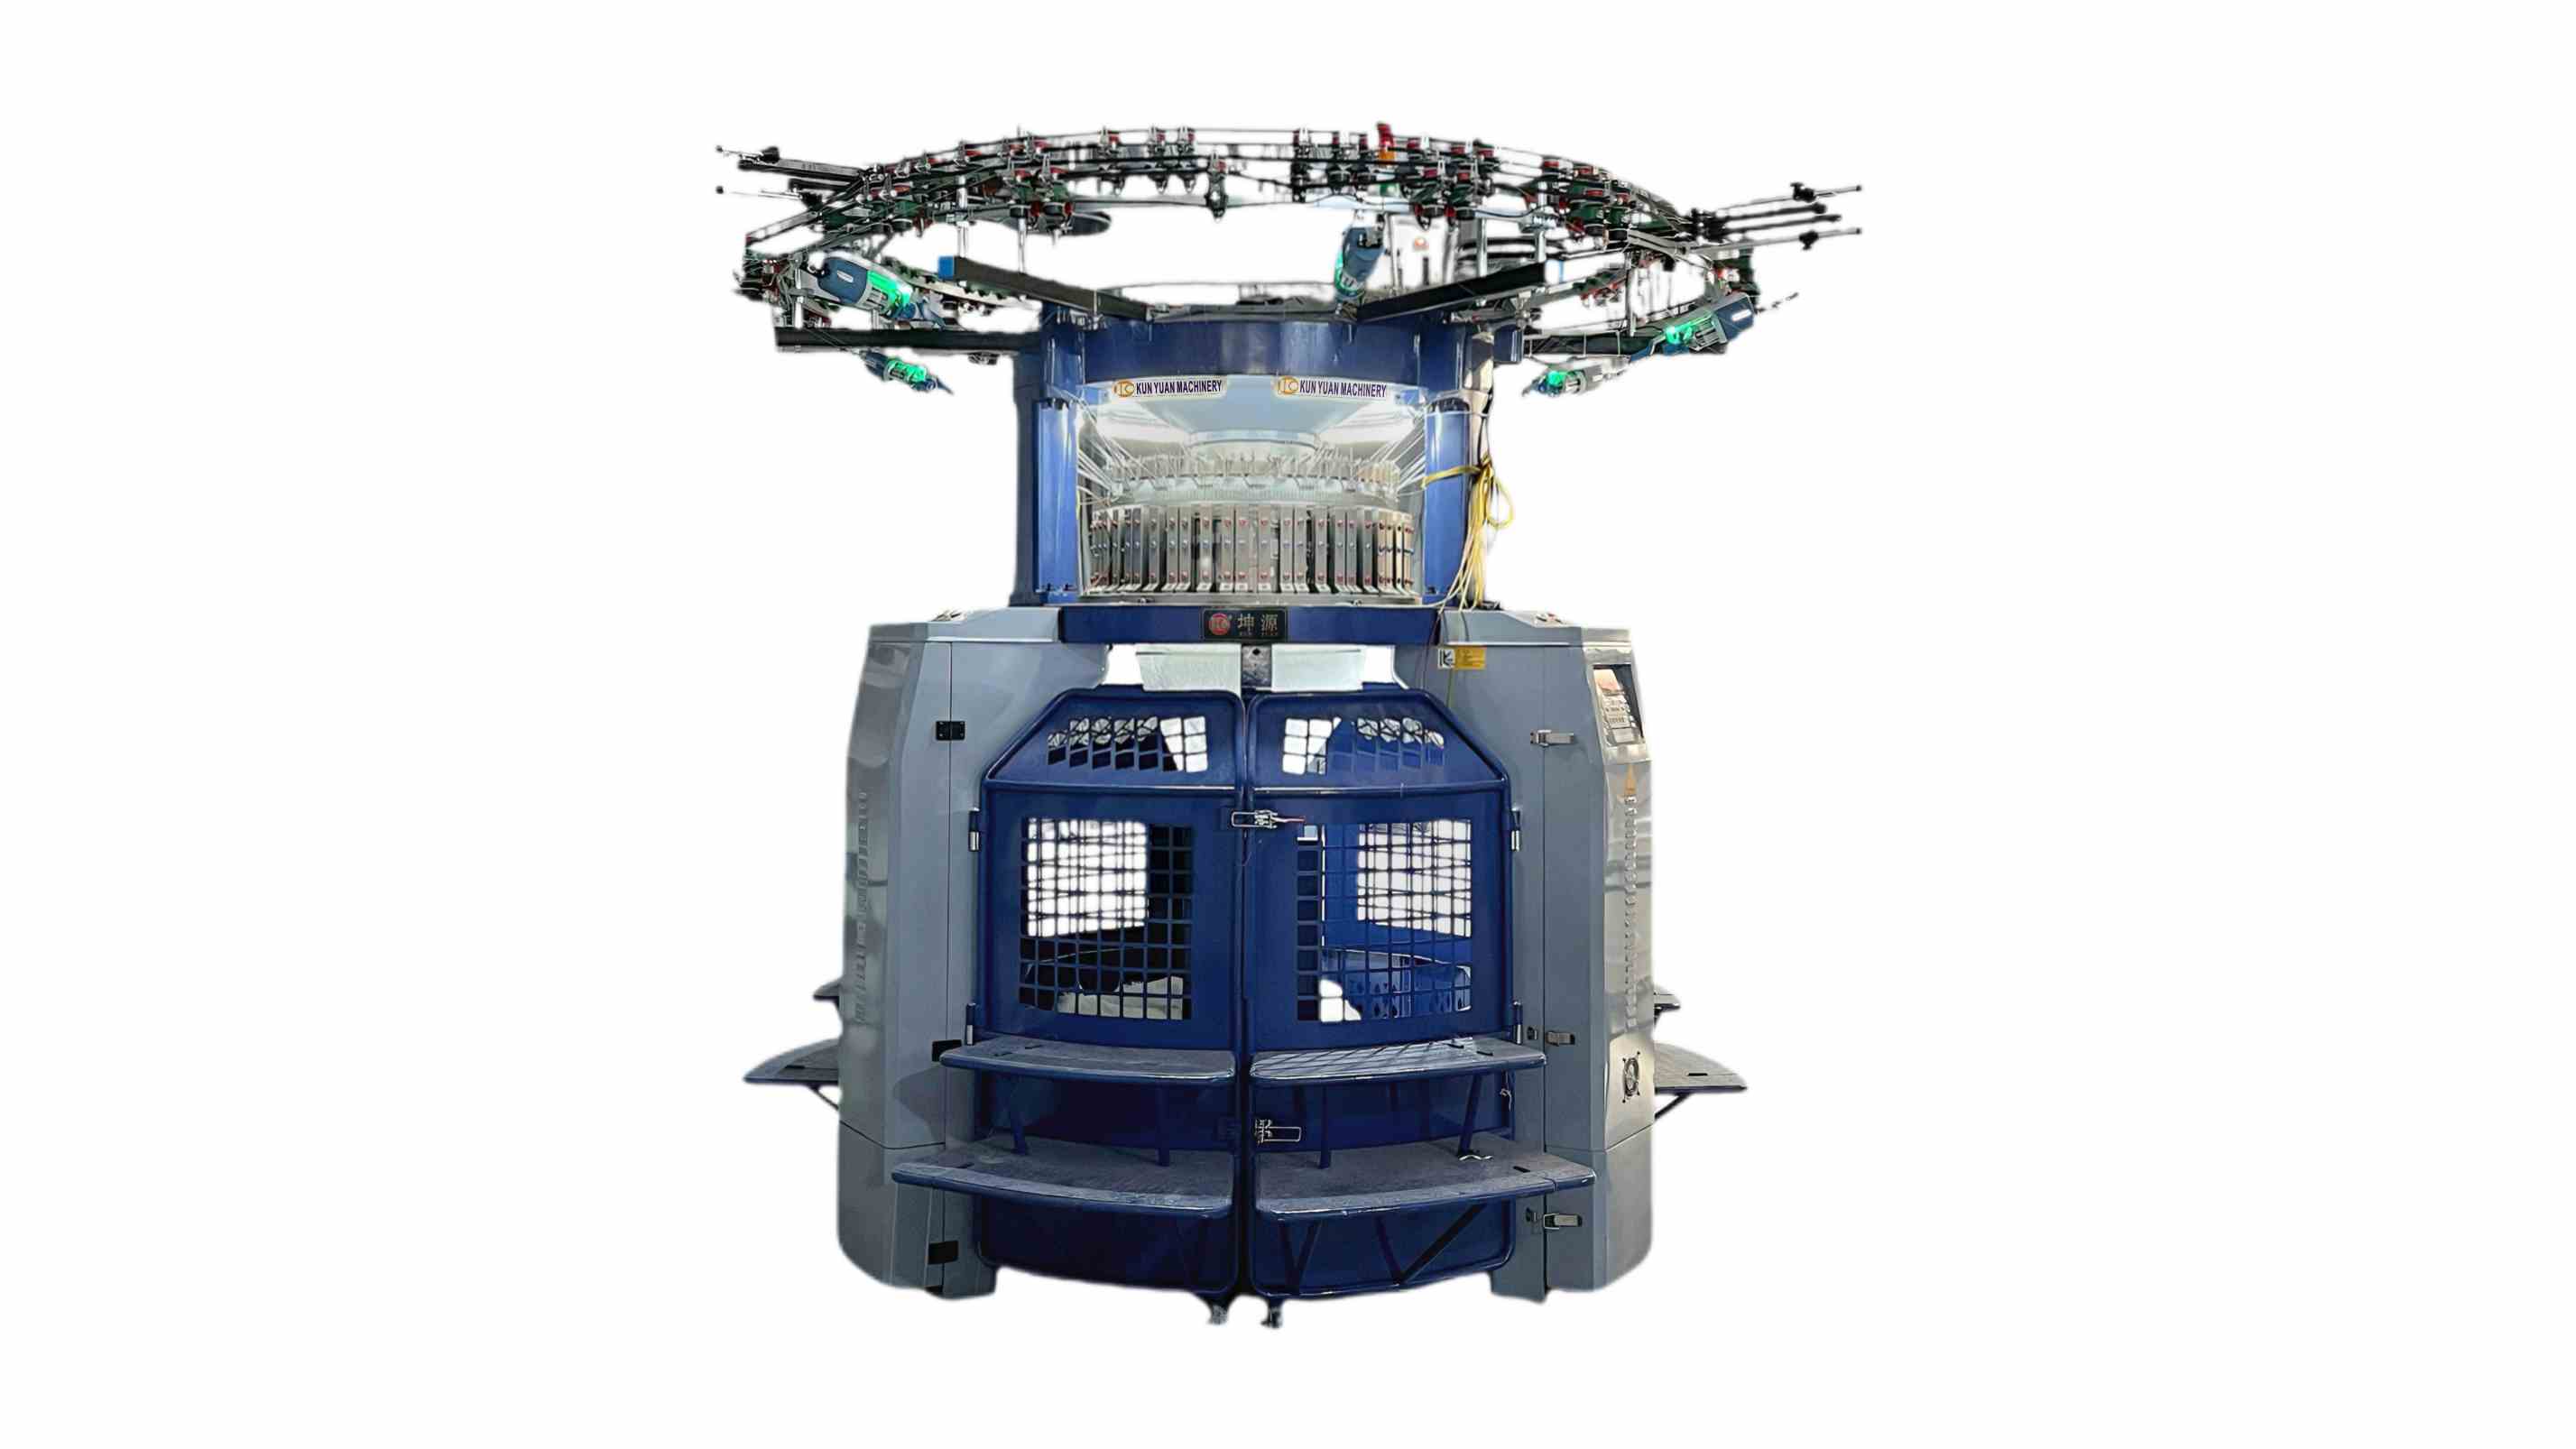
How to Choose a Towel Knitting Machine: Loop Height, Yarn and Output

Author:KUNYUAN Machine Manufacturer TIME:2026-08-30

MENU
Towel conversion cost stack

Value the machine through the towel loop that survives finishing and becomes accepted output

Terry machine selection begins with a saleable towel surface, not the tallest loop or fastest panel reading. Ground stability, pile yarn, loop distribution, wet processing and accepted yield belong in the same cost record.

Official manufacturer sources show that terry is configuration-specific. Pailung lists named KSP terry routes and publishes a KSP-OP document with model-specific gauge, diameter and feeder information. Its high-speed article gives a pile-height example for one KSP PLUS configuration, while Fukuhara lists several pile and terry architectures, including striper and electronic variants. These examples demonstrate variety; none supplies a universal loop-height range, yarn recipe or output for every towel machine.

Build a cost stack around one towel brief. State whether the end product is bath towel, bath mat, robe fabric or another defined article, then approve loop face, ground, yarn roles, finished dimensions, weight, absorbency or surface test, dimensional behavior and finishing route. Quote the exact build, run buyer yarn, mark the roll and carry it through scouring, dyeing, cutting, shearing or the agreed process. Compare accepted finished fabric per scheduled time after setup and losses, with parts and support risk visible.

01

Cost band A: define the towel surface before paying for loop capability

Convert the product into measurable greige and finished targets. Record which side carries loops, intended loop character or range, ground visibility, width, weight, end-use hand, dimensional limits and required tests. Specify whether loops remain intact, are cut for velour, receive shearing or pass another surface treatment. Use retained commercial references rather than adjectives such as plush or premium.

Ask each supplier to map that target to one machine architecture and delivered setup. A published pile-height example can frame a question but cannot become the acceptance range for another model, gauge, yarn or finish. Identify every promised pile, plating, pattern or color function as standard, optional or excluded. This band prevents an attractive finished swatch from concealing a weak ground or undocumented downstream operation.
02

Cost band B: separate ground and pile yarn duties through knitting and finishing loss

Create a yarn schedule with material, count convention, lot, package, route and structural duty for ground and pile systems. Add elastomer, binder or color roles where applicable. The trial record should show delivery positions and roll events without publishing a generic threading sequence. Inspect missing loops, streaks, pile distribution, backing stability and both fabric faces at fixed coordinates.

Track material from packages to finished disposition. Include startup fabric, tuning, held zones, laboratory samples, wet-process loss, shearing or cutting loss and rejected towel area. A heavier roll or longer greige loop does not guarantee higher accepted yield. Matched coordinates reveal whether a surface shortfall started at yarn delivery, loop formation or downstream treatment.

03

Cost band C: convert speed and roll weight into accepted finished output

Use a timed production ledger. Record scheduled minutes, setup, warm-up, stable knitting, stops, manual intervention, gross roll weight, held fabric and the quantity entering finishing. Mark at least one normal stop and restart because loop stability around events affects saleable yield. Do not combine data from different diameters, gauges, pile settings or models.

After the full process, report accepted kilograms, metres or towel pieces under a defined basis. Add energy, water and finishing data only when measured for the actual route. The most useful comparison may be accepted output per scheduled hour, but it remains conditional on the named towel, machine and mill. Preserve assumptions beside the figure so it cannot migrate into a universal capacity promise.

04

Cost band D: expose changeover, wear-part and service ownership

Choose a representative change in loop effect, yarn, color or towel weight. Measure cleaning, yarn loading, setting verification, trial fabric and time to first accepted section. If the portfolio requires striper, jacquard or velour functions, test those exact options on the quoted build. A flexible machine earns value through repeatable transition evidence, not a long family brochure.

List critical needles, sinkers, pile-forming elements, yarn-delivery items, controls and take-down components using model-specific part numbers. Add warranty, training, backups, remote support conditions and response ownership. Cost the consequence of an unavailable critical part rather than assuming lifetime service. Release the commercial stack only after receiving staff repeat the approved towel and can find the recovery records.

Terry towel fabric showing labelled ground and pile yarn faces
The surface brief separates commercial towel intent from a generic pile claim.
Marked towel knitting trial roll inspected for loop height and missing loops
Roll marks preserve loop evidence before wet and mechanical finishing alter the surface.
Finished towel samples reconciled with output, loss and changeover records
Accepted finished output closes the ledger after every loss category is counted.

Towel knitting machine cost and acceptance ledger

Cost bandEvidence basisHidden exposureRelease point
SurfaceConditioned towel and loop briefModel example treated as universalNamed build reproduces reference
Yarn and processGround/pile map plus marked finishLoss assigned to wrong layerCoordinates survive processing
OutputScheduled-time balanceGross roll replaces accepted yieldFinished total reconciles
RecoveryChangeover, parts and supportDowntime dependency omittedReceiving team repeats job

Towel machine loop, yarn and output questions

Is a higher loop always better for towels?

No. The target depends on towel use, yarn, ground stability, surface treatment and finished tests. Approve a conditioned reference rather than height alone.

Why keep ground and pile yarn records separate?

They perform different structural duties and can create different defects, losses and replacement needs.

Can manufacturer pile-height data be used for every model?

No. Treat published values as model-specific examples and request confirmation for the exact diameter, gauge, setup and yarn.

Which output figure is useful?

Use accepted finished output per scheduled time with setup, holds, wet-process loss and rejection visible.

What should the towel trial retain?

Keep machine identity, yarn lots, event marks, greige and finished samples, output ledger, changeover record and open support items.

Conclusion

A towel machine earns its value when a controlled yarn architecture forms a stable ground and pile that survives the intended finish. Costing the surface brief, material loss, accepted output and recovery route prevents peak speed or a model-specific loop claim from deciding the purchase alone. The retained towel, ledger and changeover record then provide a reproducible production baseline.

Use the four-band cost stack when requesting a buyer-yarn trial for the Towel Knitting Machine and require all loop and output claims to identify the exact configuration.

Need Help?
Please leave your contact information to get our latest catalog
Get In Touch Now >
Kunyuan Machinery Manufacturer

Tel: +86-13859034518

Email: info@kunyuanmachine.com

MP/WhatsApp: +86-13859034518

Manufacturer Address:Bacuo Village, Yonghe Town, Jinjiang City, Fujian Province

NEW KEYWORD

About Us

Products

Information